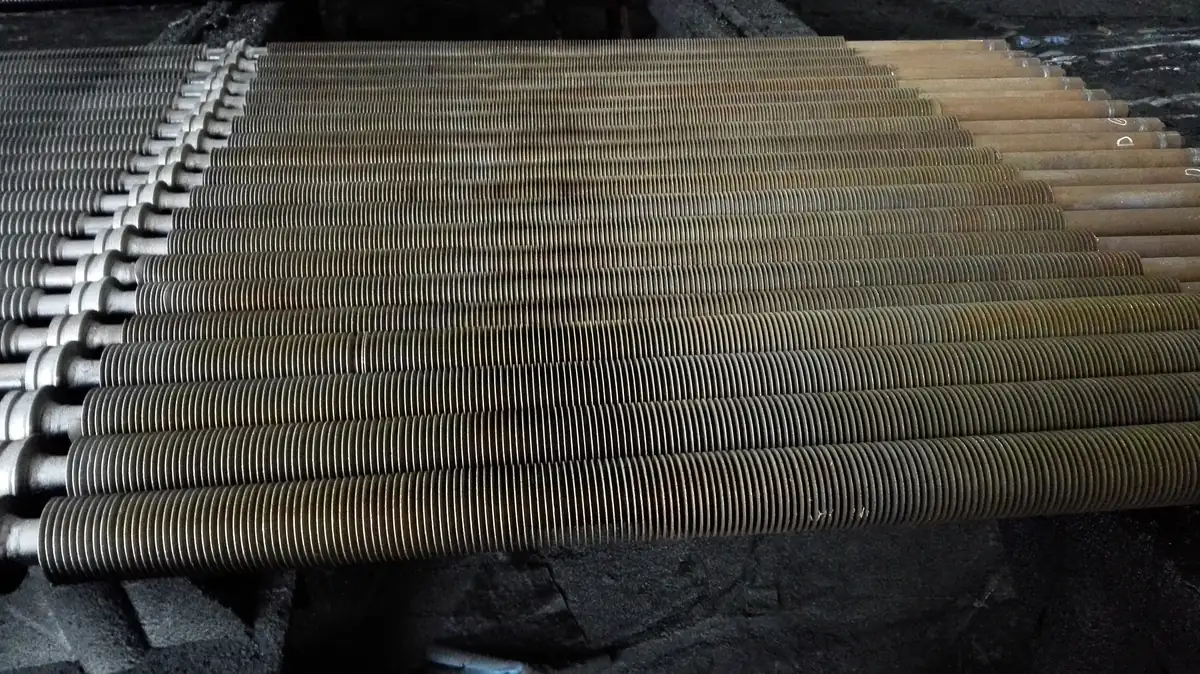
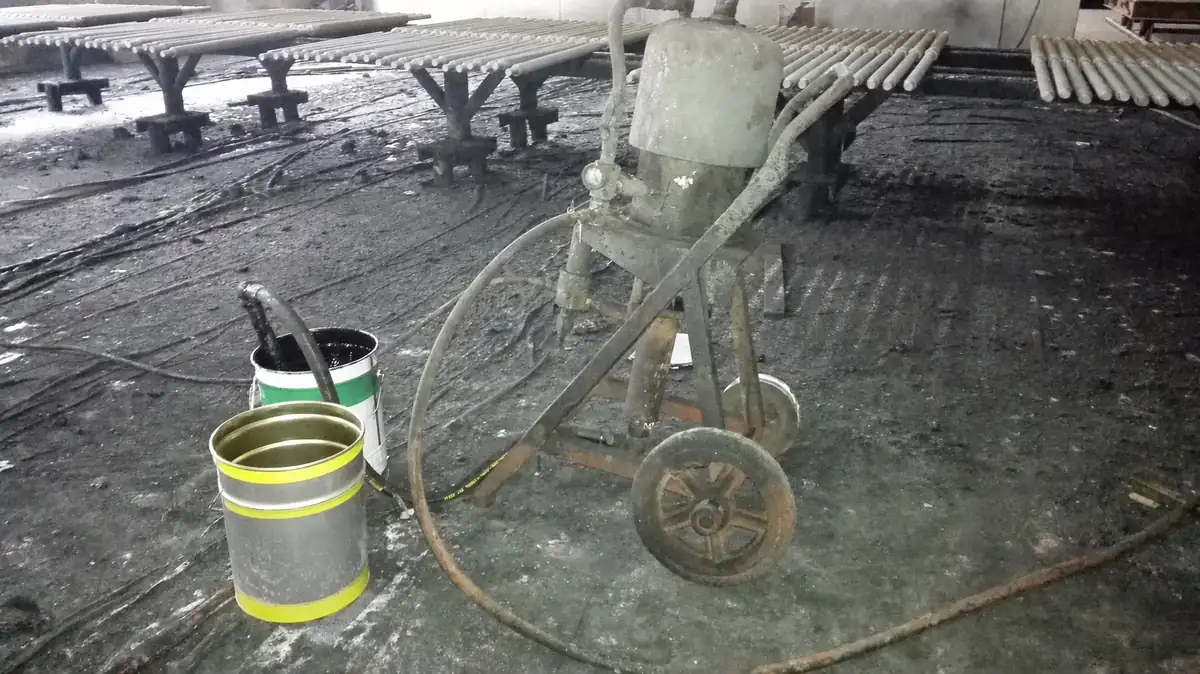
Spray equipment beside spiral-finned heat pipes in a workshop

Case Studies

Flue-Gas Heat Exchanger Corrosion Protection Application

Heat-Recovery & Environmental EquipmentSpiral-finned air-preheater heat pipes

Equipment background

This application documents corrosion-protection work on carbon-steel, spiral-finned heat pipes used in an air-preheater assembly. The narrow spacing and large finned surface make preparation, rotation and spray access central to the application plan.

Industry
Heat-Recovery & Environmental Equipment
Equipment
Spiral-finned air-preheater heat pipes
Substrate
Carbon-steel heat pipes

How the problem develops

Environmental exposure

The documented exposure is moisture-bearing corrosive flue gas around carbon-steel finned tubes. Temperature values in the source are not reconciled, so no definitive project temperature is published here.

Operating conditions

The application record focuses on coating access around closely spaced fins and on limiting the time between steel preparation and coating. It does not establish a public power-plant operator, operating result or service history.

Observed condition and failure signs

A corrosion-protection requirement for the flue-gas-exposed heat pipes is documented. The record does not independently quantify corrosion loss or demonstrate particle-erosion damage to an installed coating.

Problem analysis

Spiral fins increase the surface area and create narrow reverse-side zones. Preparation residue or incomplete spray access in those zones can interrupt continuity, so the tubes were handled in stages and rotated to expose each side for application and inspection.

Problem to address

The source describes moisture-bearing flue gas with acid-forming species. That supports a corrosive-exposure mechanism, but it is not a project-specific condensate chemistry measurement or a measured corrosion-rate result.

Protection objectives

Prepare and cover the carbon-steel tube and fin surfaces continuously while keeping the completed geometry practical to inspect. This is an application objective, not a claim of verified service performance.
Solution approach

System selection rationale

The source documents a corrosion-protection coating application but does not verify a current DAYU-X product model. Any present-day material selection must be reviewed against confirmed gas composition, moisture, temperature, steel condition and application access.

Surface preparation

Remove oil, rust and scale from the carbon-steel heat pipes and blast the specified work surface to Sa 2.5. The source also describes local repair preparation; prepared surfaces should be cleaned before staged spraying begins.

Application workflow

Identify and arrange the finned tubes, complete blast preparation, remove residual dust, spray the accessible surfaces, rotate the tubes for the reverse side, and inspect coverage across the full fin geometry. No unreconciled coat count or thickness is presented as an as-built fact.

Curing and return-to-service control

Protect the coated tubes from impact and contamination during handling. Release or installation should follow the selected system's approved curing instructions and a completed surface inspection; no commissioning result is claimed.

DY-13 is technically relevant to flue-gas corrosion review; this link does not identify the product used in the documented application. Selection depends on confirmed project conditions.

Application and quality control

Inspection should confirm the prepared steel condition, cleanliness inside fin gaps, reverse-side coverage after rotation and a continuous visible finish. Exact dry-film thickness is omitted because the available source values conflict and no reconciled as-built record was found.

Inspection and maintenance

Future inspections should compare the same fin roots, tube surfaces and handling points for corrosion, contamination or local coating damage. No service interval or corrosion-reduction result is inferred from the application photographs.

Site-condition images

The photographs show the spiral-finned heat pipes, preparation and coating stages. They do not establish a current product identity or an operational performance result.

Frequently asked questions

Why is fin geometry important during spray application?

Closely spaced fins create reverse-side and root areas that can be missed unless tube position, spray angle and inspection are controlled.

Does this page verify acidic-condensate chemistry?

No. The source supports moisture-bearing, acid-forming flue-gas exposure, but it does not provide a project-specific condensate analysis.

Do the photographs verify the current coating product?

No. They document equipment and application stages; no readable current DAYU-X product identity is established.

Why are temperature and thickness values omitted?

The available records do not provide reconciled project values suitable for publication as definitive as-built conditions.

DAYU-X

Have a project with similar operating conditions?

Share the equipment, exposure and current damage so we can compare the relevant application direction.

Contact technical team