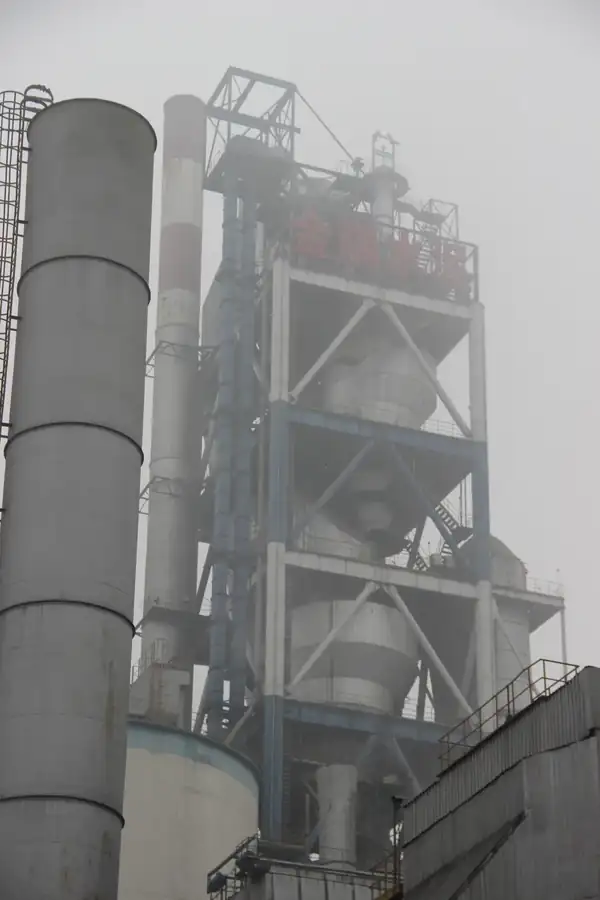
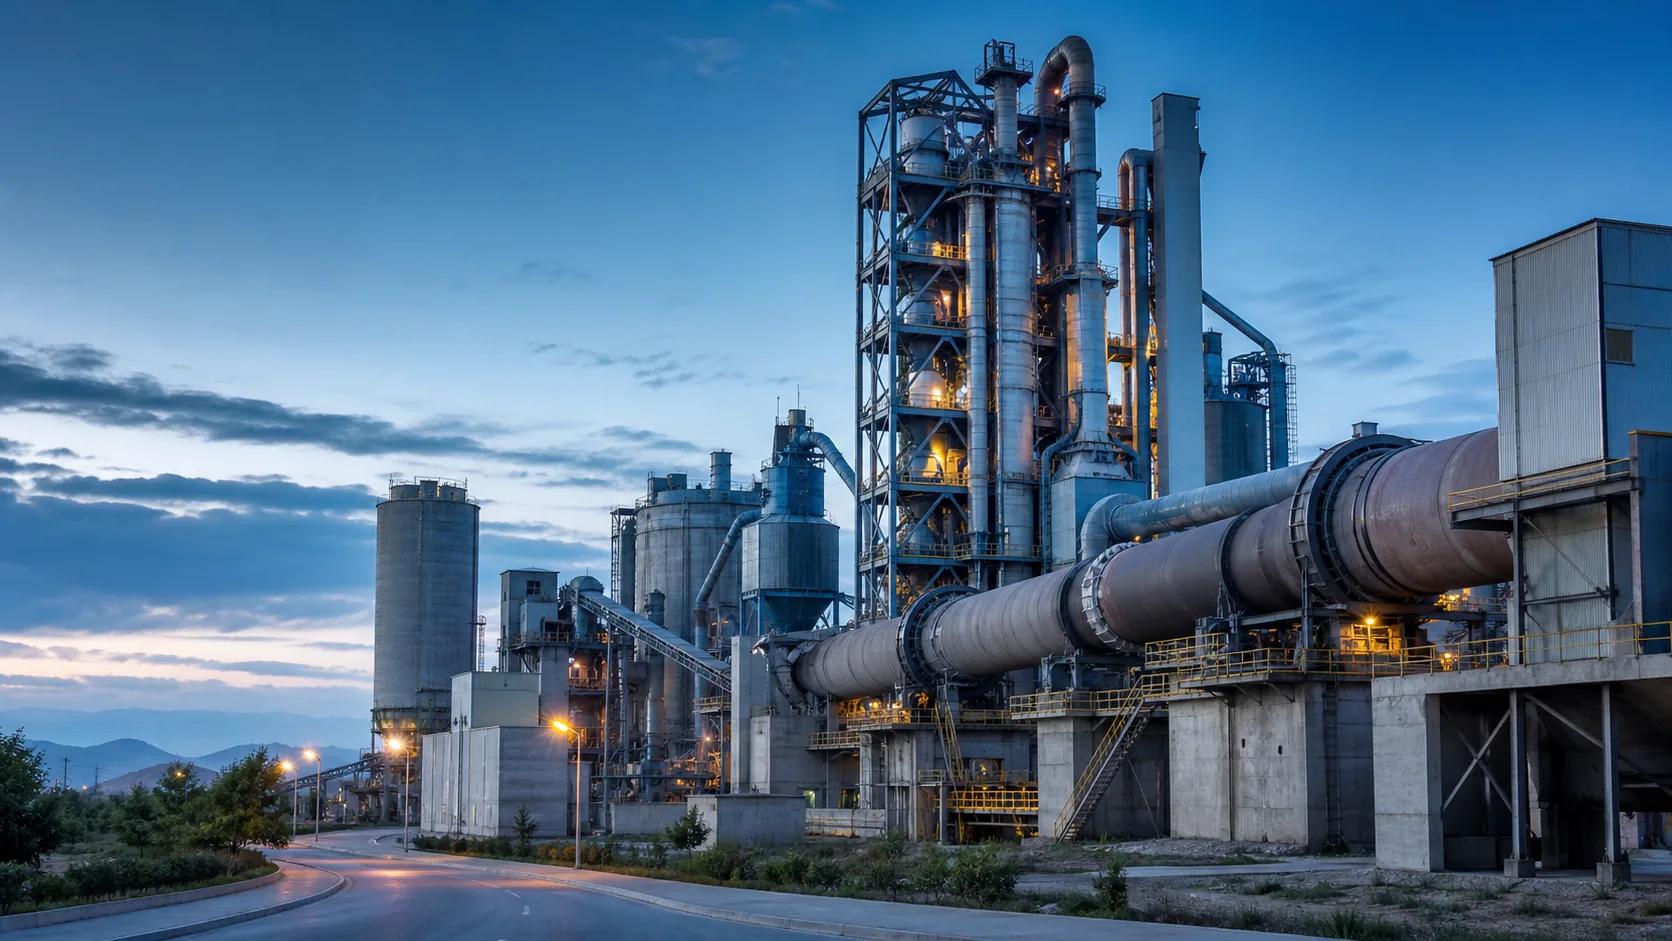
Cement industrial equipment

Industry applications

Industrial Coatings for Cement Plants

Follow the cement process from material transfer to the kiln and downstream gas path. Each zone needs a different assessment of abrasion, heat flow and maintenance access.

A production line with different protection needs

Raw-material preparation, calcination, cooling, grinding and dust collection connect equipment with very different surface exposures. A kiln-shell insulation decision cannot be transferred directly to a hopper or a dust-laden bend.

Start with the location of the problem in the process: contact with moving solids, exposure to hot gas, or heat leaving an external surface. This separates the protection objective before a coating system is considered.
Plan work around the shutdown window

Rotating equipment, dusty access routes and continuous production constrain inspection and application. Record where cleaning, surface preparation and curing can actually be completed during the available stop.

Route by cement-plant equipment

Separate solids, gas and shell conditions

Material and gas routes

Describe the mineral dust, where it changes direction, and whether a surface sees sliding material or direct impact. A local groove at a bend needs a different investigation from widespread oxidation along a hot duct.

Kiln operation and heat flow

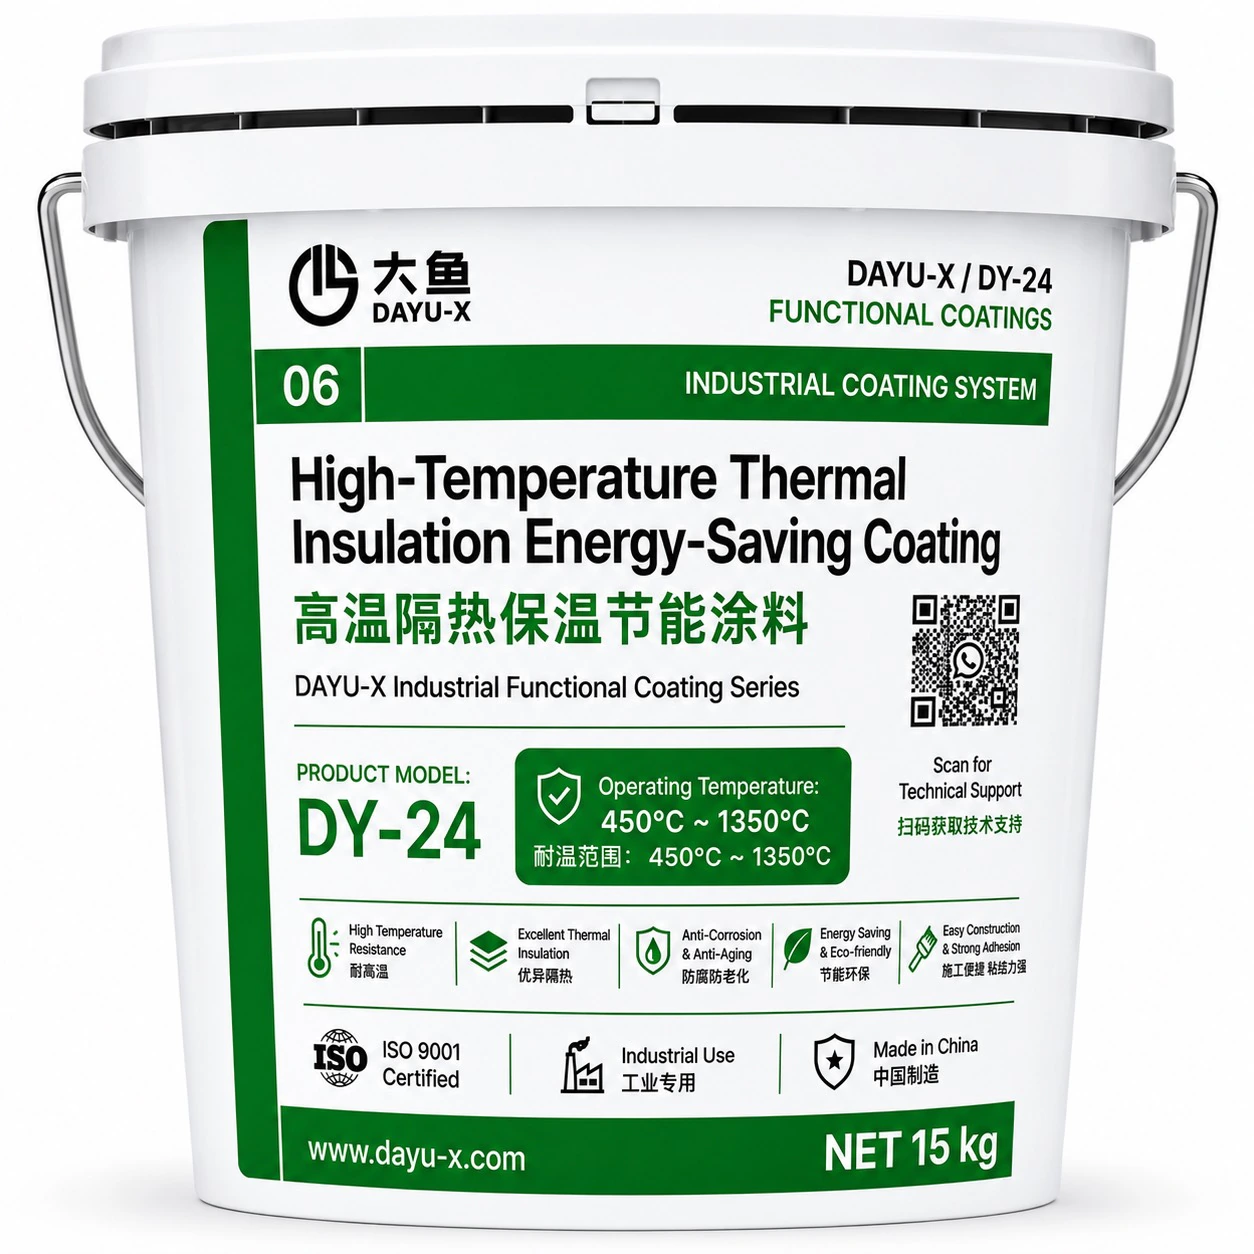
Review shell condition, thermal cycling, existing insulation and access around the rotating kiln. Surface-temperature observations should be interpreted with the process operating state, not as a stand-alone energy-saving result.

Read the damage pattern before choosing a system

Wear concentrated at transfer points

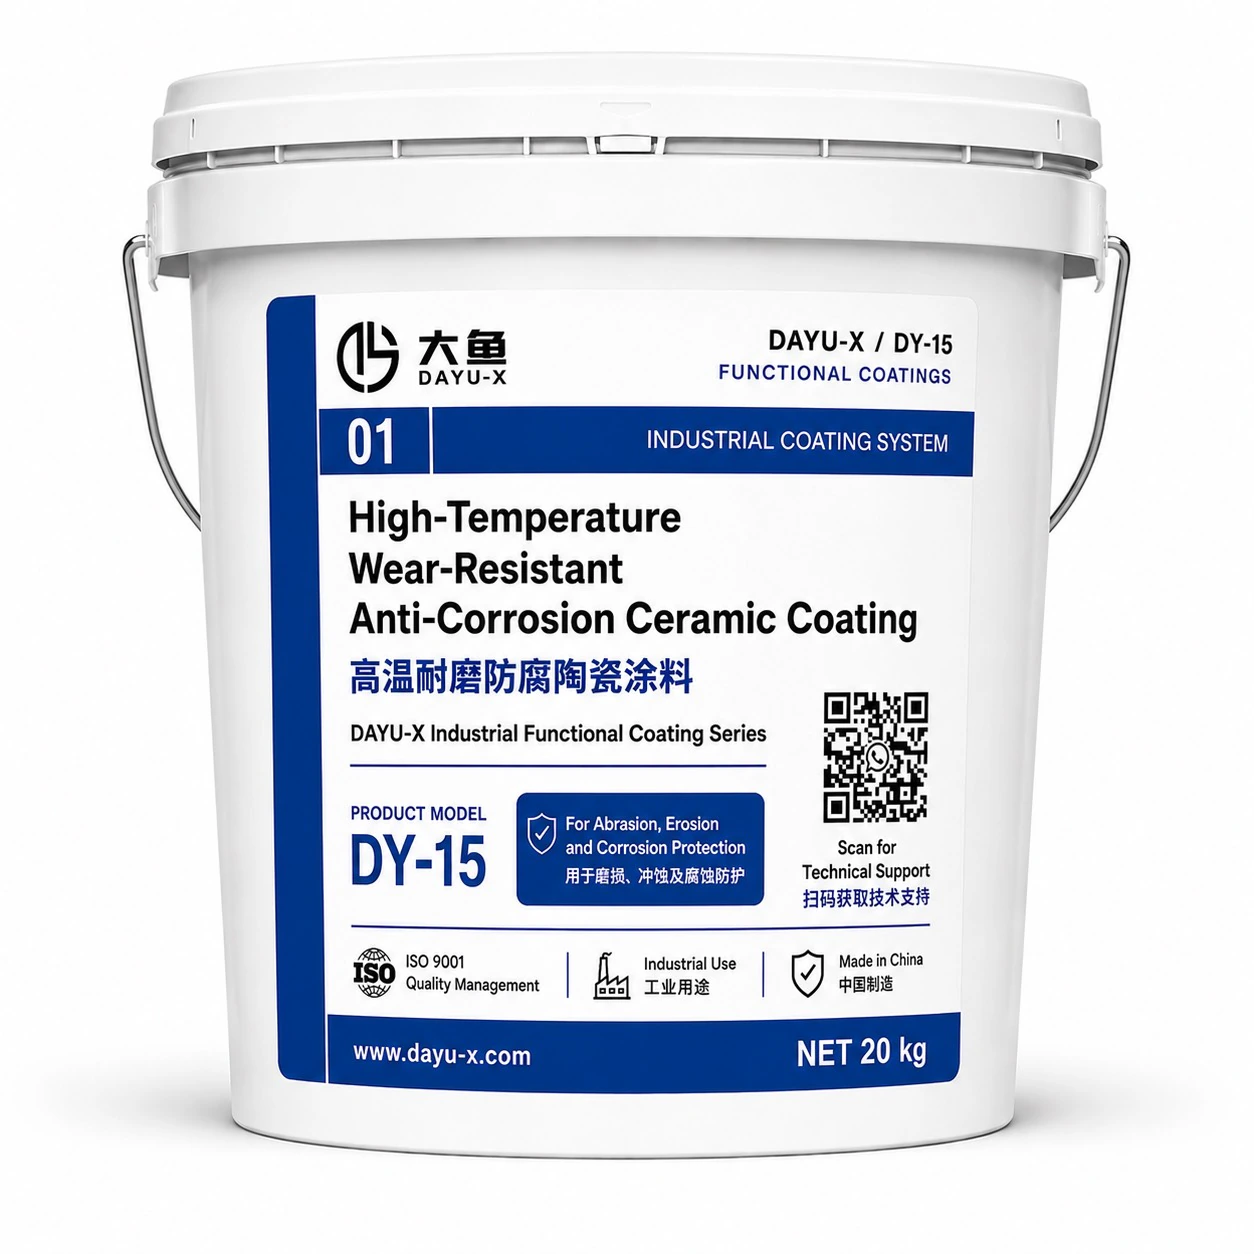
Hoppers, chutes and conveying transitions concentrate mineral contact. Map the damaged face and flow direction so protection is directed at the exposed area rather than applied uniformly without a wear assessment.

Review wear and erosion protection

Hot-gas surface deterioration

Heat, local gas atmosphere and cycling can affect kiln-adjacent steel and gas ducts. Distinguish corrosion or oxidation from mechanical removal by dust; a temperature label alone does not identify the dominant mechanism.

Review hot-gas corrosion conditions

Heat loss around the kiln shell

Exposed areas, damaged insulation and changes in geometry interrupt the thermal layer. Review the existing shell and the complete insulation arrangement before treating a coating as a replacement for the underlying repair.

Review cement-kiln insulation planning

Prepare a cement-line protection brief

Identify the process stage and exact surface, then supply photographs showing both the damaged area and its surroundings. Include material-flow direction, known operating conditions, substrate or lining type and the available shutdown sequence.

  • For handling equipment: describe dust, impact locations and remaining substrate condition.
  • For the kiln: separate refractory-side work, shell protection and external insulation objectives.
  • For every proposed repair: identify cleaning access and the time available before restart.
Discuss this equipment and operating brief

Questions about this industry application

Can one coating cover every cement-plant duty?

No. Material handling, kiln refractories and external shell insulation perform different functions. Route each surface by its actual exposure and required protection function.

What should be recorded at a worn hopper?

Record the flow direction, impact or sliding zones, particle information and substrate condition. Include a wider photograph so the damage can be placed within the transfer arrangement.

Is kiln-shell insulation the same as a refractory coating?

No. Shell insulation addresses a thermal path at the shell, while a refractory-side functional layer has a different location and purpose. The complete kiln arrangement must be reviewed.

Does a hot duct always need a wear system?

Not necessarily. Dust erosion and hot-gas corrosion can coexist, but their relative importance must be established from the damage pattern and operating information.

What limits application during a cement shutdown?

Access around equipment, residual heat, dust removal, surface preparation and the permitted curing sequence determine whether the proposed work can be completed before restart.

Does the cement case prove a particular saving?

The linked case provides application context. It should not be read as a quantified energy-saving guarantee or as confirmation that all systems on this industry page were installed.

DAYU-X

Discuss an application in your industry

Tell us the equipment, process environment and current problem. We will help organize the next technical review.

Contact technical team